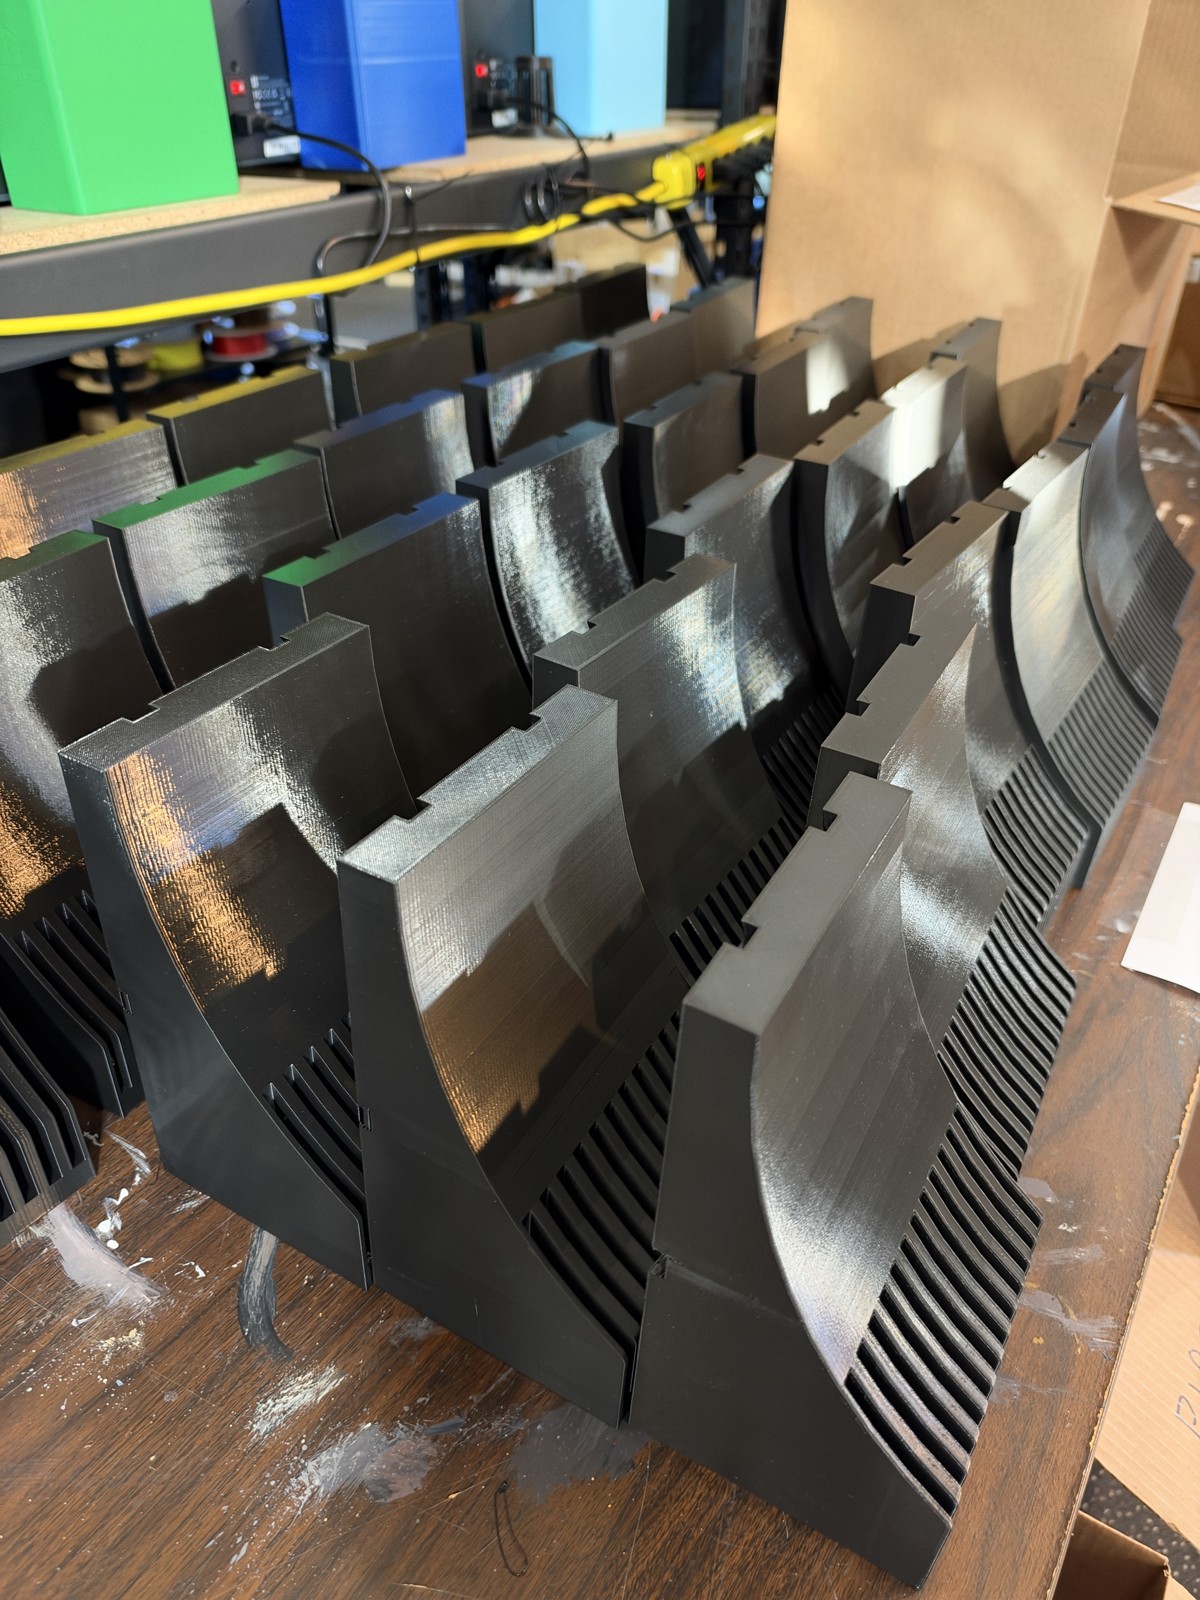
Mass production of a part is SOO much different from going for a single print. We have to optimize for failure rate, printer efficiency, the work hours available to rotate the machines, and post-processing requirements.
One print setting can EASILY cause hours of extra labor. Bad support settings are a major thing we've seen. For critical pieces that could fail, we generally slow the print way down, bump up the first-layer temperatures, and add a brim.
Printing one part is WAY different from printing hundreds.
Polymaker came by the studio last week, and we're currently testing its new PETG formula. I'm hopeful that it will be better and produce less stringing than the old PETG, but testing is still underway.
There's some confusion around the packaging. My understanding is that Polymaker may still use some of its old packaging without relabeling it for the new formula.
During testing, we're paying attention to humidity and using a PolyDryer.
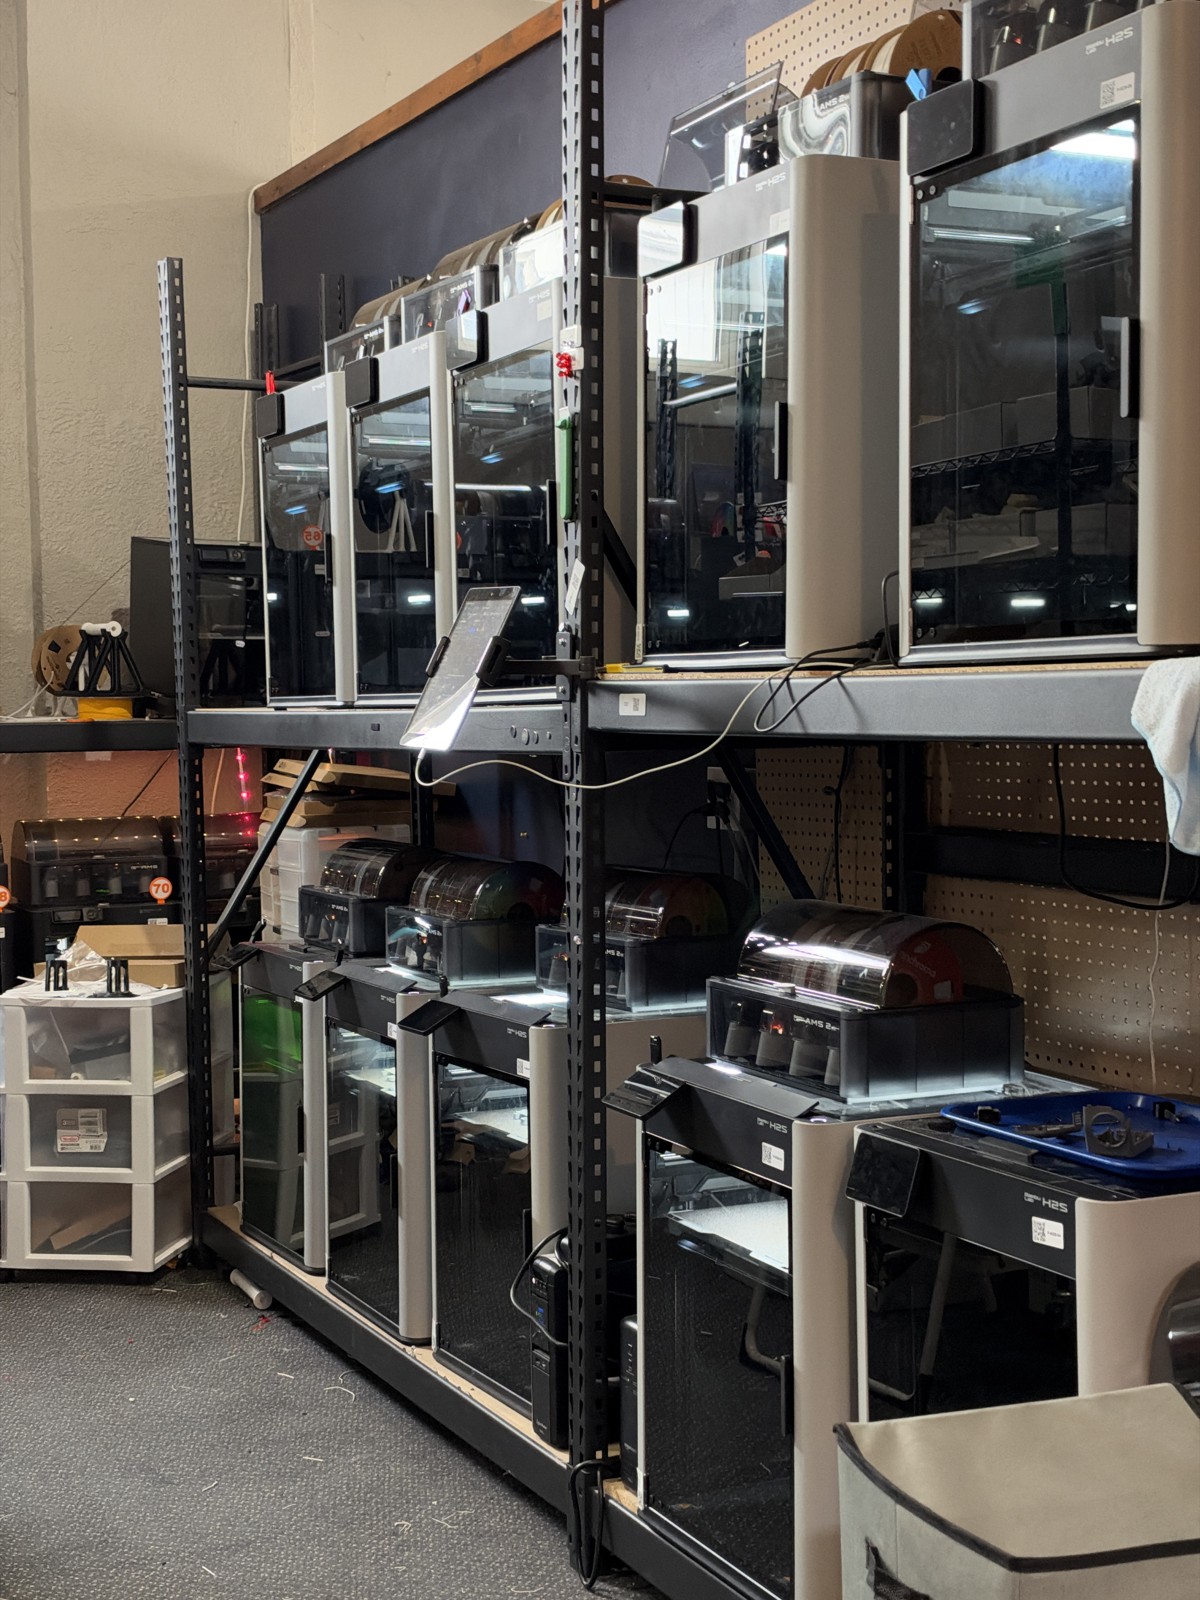
We're expanding the H series fleet at the JC print farm to help meet demand for larger-format prints. We've noticed that many companies that can buy only one printer for a department are choosing H series printers right now.
The Bambu fleet is our preference for now, although we've seen other machines catching up and may consider alternatives to the H series. I found the H2D expensive, and we like the H2S at the moment.